
Dairy Processing · UHT
UHT Unit: Tubular UHT Plants for Long-Life Dairy Products
Heat for seconds, store for months: a Protrus UHT unit makes milk, cream and beverages commercially sterile for aseptic packaging and ambient distribution.
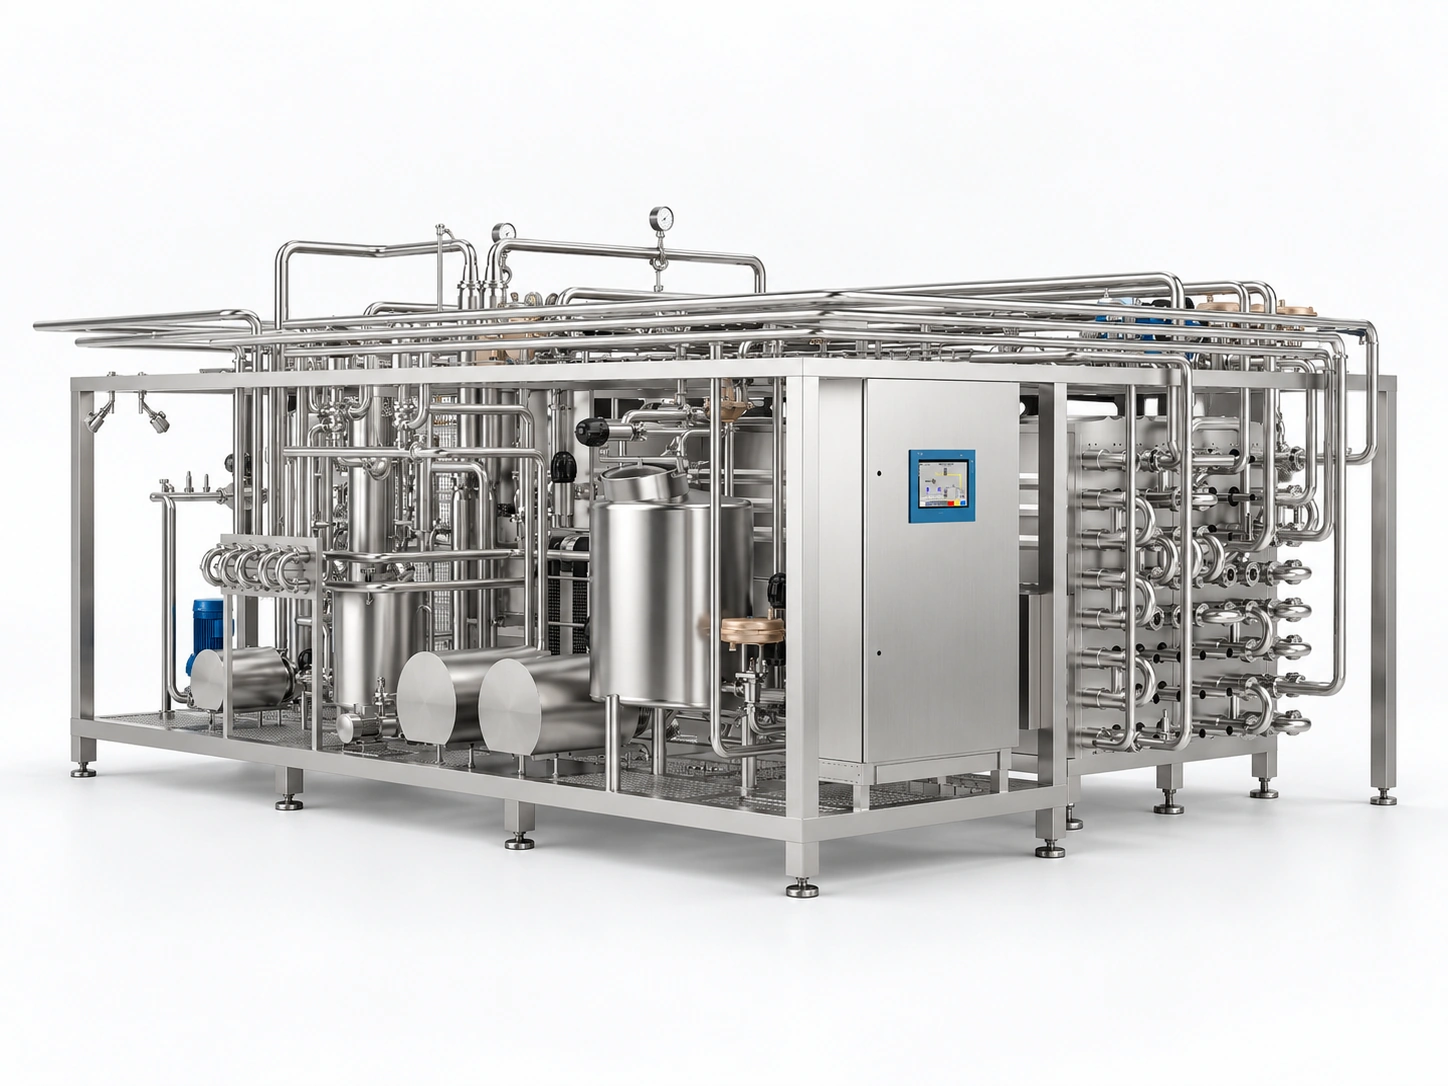
Protrus UHT unit: tubular heat exchanger banks, hot-water module, balance tank and control panel on one frame.
Indirect tubular heating
Product never touches the heating medium
Wide flow channels
Cream, cocoa milk, plant-based and protein drinks
Factory-tested skid
Homogenizer, holding tube, hot water, CIP and PLC
Sterility record
B* and C* calculated for every batch
Commercially Sterile Milk, Cream and Drinks Without Refrigeration
Ultra-high-temperature (UHT) treatment heats a liquid food to 135–150 °C (275–302 °F) for a few seconds and cools it again immediately. This short, intense step destroys vegetative bacteria and heat-resistant spores while keeping color, flavor and nutrients close to fresh pasteurized milk. Filled aseptically, the product keeps for 6 to 12 months without refrigeration.
The Protrus UHT unit is an indirect tubular system: the product never touches the heating medium, heat is transferred through stainless steel tube walls, and up to 90 % of the energy is recovered by product-to-product regeneration. It is delivered as a factory-tested skid with homogenizer, holding tube, hot-water circuit, CIP and automation ready to connect.
137–145 °C
sterilization, 2–6 s holding (279–293 °F)
1,000–30,000 L/h
capacity per line (265–7,900 US gal/h)
85–90 %
heat recovery by regeneration
6–12 months
ambient shelf life after aseptic filling
Why Tubular UHT?
Tubes have no gaskets in the product path and tolerate high pressure, so a tubular UHT unit runs reliably at sterilization temperature for long production runs.
The wide flow channels handle products that would block a plate heat exchanger: cream, flavored milk with cocoa or stabilizers, plant-based drinks with fibers, and high-protein formulas.
Product, hot water and cooling water flow in counter-current, so the temperature difference on the hot side stays small and burn-on is kept to a minimum.
UHT Heating Technologies Compared
| Indirect tubular (Protrus focus) | Indirect plate | Direct injection / infusion | |
|---|---|---|---|
| Heat transfer | Through tube walls, hot water | Through thin plates, hot water | Culinary steam mixed with product |
| Heat recovery | 85–90 % | Up to 90 % | 40–50 % |
| Run time | Long: 10–20 h for milk | Short, fouling sensitive | Long, very low fouling |
| Best for | Milk, flavored milk, cream, plant-based, viscous drinks | Low-viscosity milk, juices | Premium milk, desserts, heat-sensitive formulas |
| Trade-off | Slightly more heat load than direct | Gaskets limit pressure and particles | Higher energy, culinary steam and flash vessel needed |
Protrus builds indirect tubular UHT units. For heat treatment below sterilization temperature, see our pasteurization and standardization line.
Final Products Made on a UHT Unit
One unit, one set of recipes in the PLC: the same plant switches between milk, cream and beverages, each with its own heating profile and homogenization.
UHT milk
Whole, semi-skimmed and skimmed milk, 0.1–3.8 % fat, with 6–12 months ambient shelf life.
Flavored milk
Cocoa, strawberry and fruit milk drinks with stabilizer dosing and a higher heat for spores.
UHT cream
Cooking and whipping cream with 10–35 % fat, homogenized aseptically after the holding tube.
Plant-based drink
Oat, soy and almond drinks from an enzyme-treated base; tube-in-tube for high fiber.

Coffee creamer
Barista and coffee creamers with a pre-hold time tuned to the protein level.
High-protein drink
Protein drinks with upstream and aseptic homogenization for a smooth texture.
Typical Recipes on a Protrus UHT Unit
| Product | UHT temperature / hold | Homogenization | Notes |
|---|---|---|---|
| UHT milk (0.1–3.8 % fat) | 137–140 °C / 4 s (279–284 °F) | Upstream, 180–250 bar | Run time 10–20 h depending on raw milk quality |
| Flavored milk (cocoa, fruit) | 140–142 °C / 4–6 s (284–288 °F) | Upstream, 180–200 bar | Higher heat for spores from cocoa and sugar; stabilizer dosing |
| Cream 10–35 % fat | 138–142 °C / 4 s (280–288 °F) | Aseptic, downstream | Aseptic homogenizer breaks fat clusters formed in the hot section |
| Plant-based drink (oat, soy, almond) | 140–145 °C / 4–6 s (284–293 °F) | Upstream, 200–250 bar | Enzyme-treated base; tube-in-tube for high fiber |
| Coffee creamer, protein drink | 138–143 °C / 4–6 s (280–289 °F) | Upstream and aseptic | Pre-hold time tuned to protein level to limit deposits |
The Tubular UHT Process, Step by Step
Thirteen steps between the balance tank and the aseptic filler, each with a defined temperature, pressure and time.
The diagram shows a typical indirect tubular UHT line for milk. Zone A brings the product gently up to temperature, zone B sterilizes and cools it, and zone C keeps it sterile until it reaches the package. Every value on the diagram is a recipe parameter in the PLC, so the same plant can switch between milk, cream and beverages.
- 1Balance tankLevel-controlled; milk at 4–6 °C (39–43 °F)
- 2Feed pumpConstant flow + flow meter
- 3Regenerative preheatingProduct/product; to 75–80 °C (167–176 °F)
- 4Vacuum deaeratorAir and off-flavor removal; optional
- 5Homogenizer2-stage, upstream; 180–250 bar (2,600–3,600 psi)
- 6Pre-holdingProtein stabilization; 90–95 °C (194–203 °F)
- 7UHT heatingPressurized hot water; to 137–142 °C (279–288 °F)
- Steps 3 and 9 form the regeneration loop: the sterilized product heats the incoming cold milk.
- 8Holding tubeInsulated, sloped; 2–6 s at 4–6 bar (58–87 psi)
- 9Regenerative coolingHeat back to step 3; to 30–40 °C (86–104 °F)
- 10Final coolingWater / ice water; to 20–25 °C (68–77 °F)
- Divert valveIf T < set point: back to balance tank, plant re-sterilizes
- 11Aseptic homogenizerCream, protein drinks; optional
- 12Aseptic tankSterile air blanket; buffer for filler stops
- 13Aseptic fillerCarton, bottle or bag; 6–12 months shelf life
- Every value on the diagram is a recipe parameter in the PLC, so the same plant can switch between milk, cream and beverages.
Steam 6–10 barHeats the closed hot-water circuit
Hot-water circuitΔT product/water only 3–6 K
Cooling and ice waterFinal cooling, homogenizer
CIP unitLye / acid up to 140 °C (284 °F)
PLC / SCADARecipes, sterility interlocks, records
Process flow of a Protrus indirect tubular UHT unit with heat recovery loop, divert valve and aseptic zone. Dashed boxes are options or the divert path; typical milk values, 1 bar = 14.5 psi.
Process Steps
Zone A · Steps 1–7
Heat-up and pretreatment
Feed and preheating (1–3). A level-controlled balance tank and a feed pump give a constant flow. Cold milk at 4–6 °C (39–43 °F) enters the regenerative section and is heated to 75–80 °C (167–176 °F) by the sterilized product flowing back.
Deaeration (4). An optional vacuum deaerator removes dissolved air and volatile off-flavors. Less air means less fouling, a more stable homogenizer and less oxidation during storage.
Homogenization (5). A two-stage homogenizer at 180–250 bar (2,600–3,600 psi) reduces fat globules to about 1 µm so cream does not rise during months of storage. The plant image shows a HOMMAK homogenizer in this position.
Pre-holding (6). A short hold at 90–95 °C (194–203 °F) stabilizes whey proteins before the hot section. This reduces protein deposits on the hot tube walls and extends the run time.
Zone B · Steps 7–10
Sterilization and cooling
UHT heating and holding (7–8). Pressurized hot water raises the product to 137–142 °C (279–288 °F). The insulated, slightly sloped holding tube keeps it there for 2–6 s. Product pressure stays above the boiling pressure, typically 4–6 bar (58–87 psi).
Cooling and divert valve (9–10). The product returns its heat to the incoming milk, then cooling water brings it to 20–25 °C (68–77 °F). If the holding temperature drops below set point, the divert valve sends the product back and the plant re-sterilizes.
Zone C · Steps 11–13
Aseptic zone
Aseptic homogenizer (11). An optional aseptic homogenizer after the holding tube gives cream and protein drinks a smoother texture.
Aseptic tank and filler (12–13). A sterile aseptic tank buffers the flow so short filler stops do not interrupt sterilization. The product then goes to the aseptic filler for cartons, bottles or bags.
Sterility and Product Quality: B* and C*
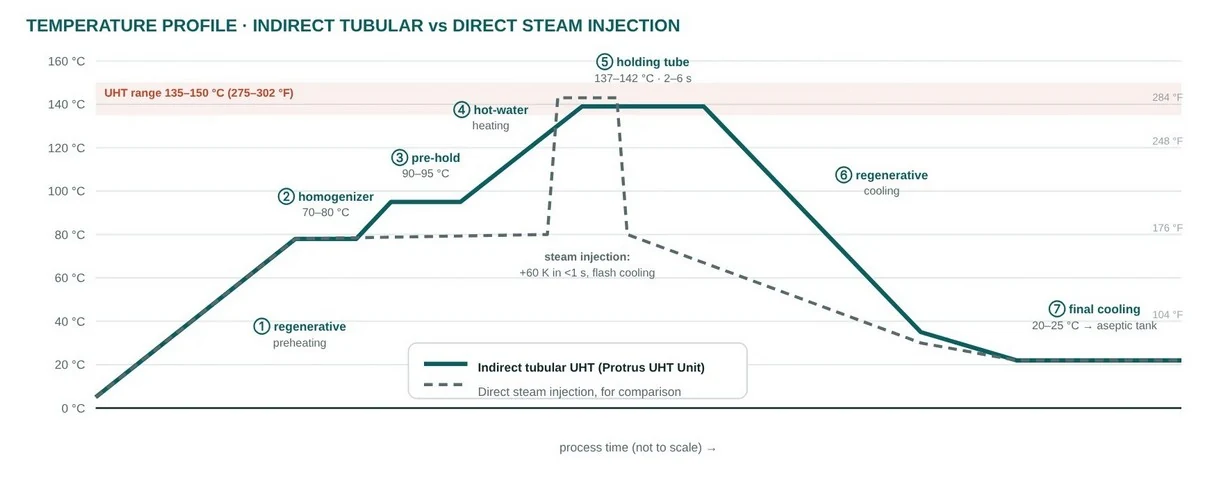
Indirect heating raises the temperature in stages and recovers most of the energy; direct steam injection heats in under a second but recovers far less.
B* expresses spore kill
A UHT recipe balances two effects. The sterilizing effect B* = 1 corresponds to a 9-log reduction of heat-resistant thermophilic spores, and commercial plants run at B* above 1.
C* describes product quality
The chemical effect C* covers cooked flavor, browning and vitamin loss; C* below 1 keeps thiamine loss under about 3 %.
The Protrus control system calculates both values from the measured temperature profile and the actual flow, so every batch has a sterility record.
Inside the Protrus UHT Unit
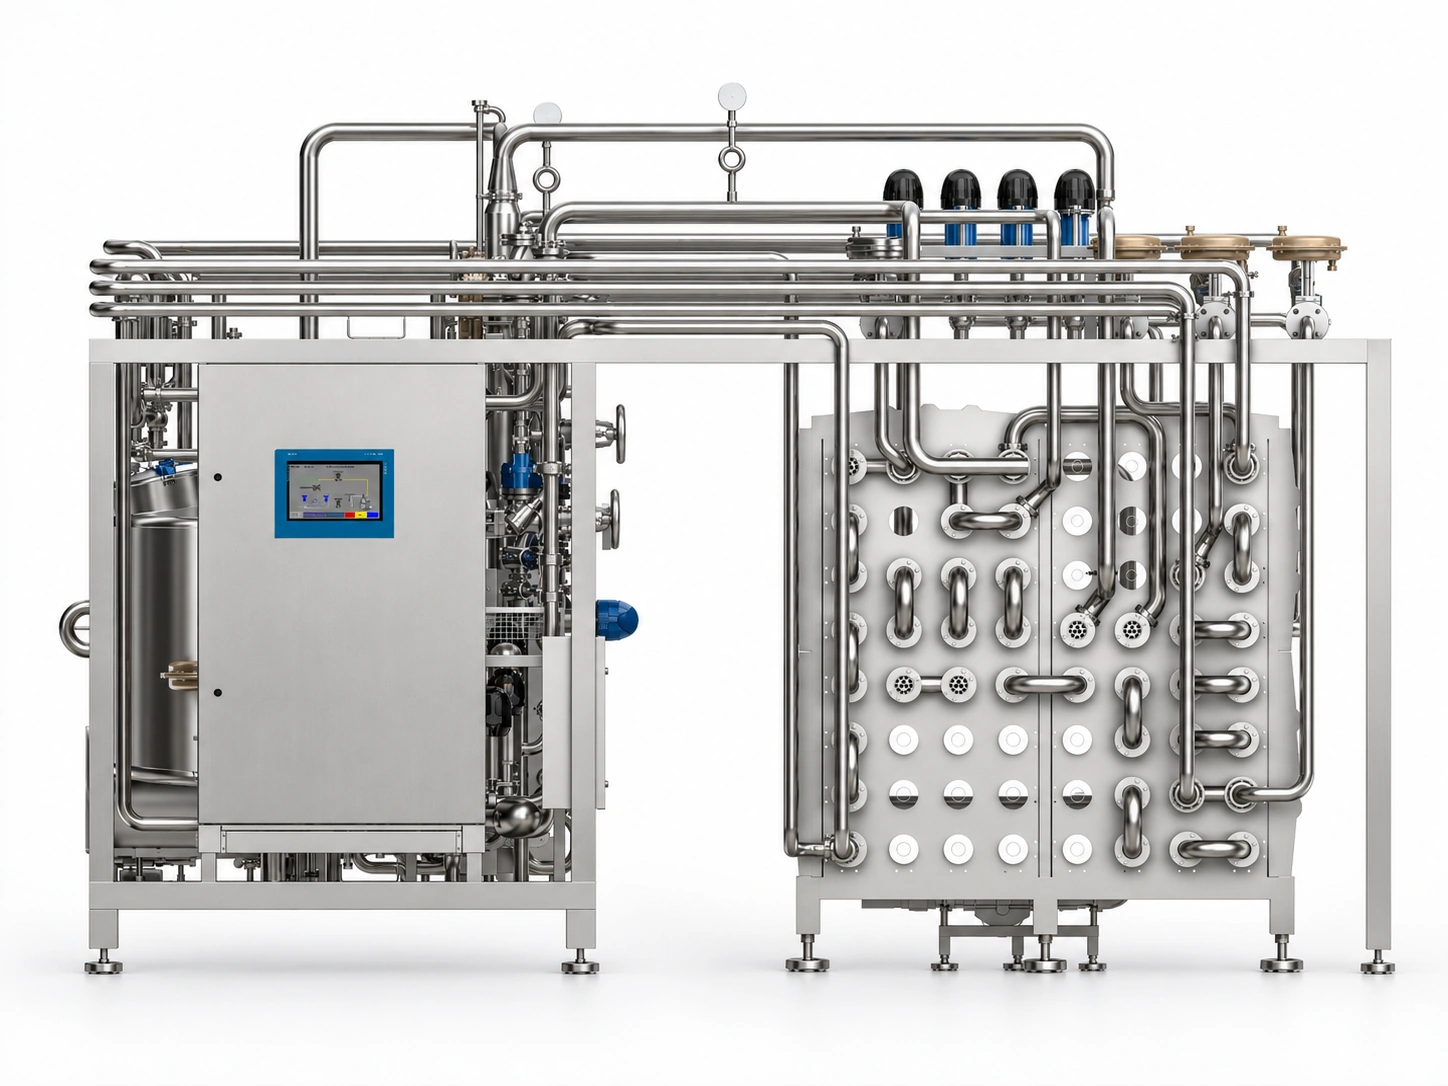
Front view: control panel and multi-tube heat exchanger bank.
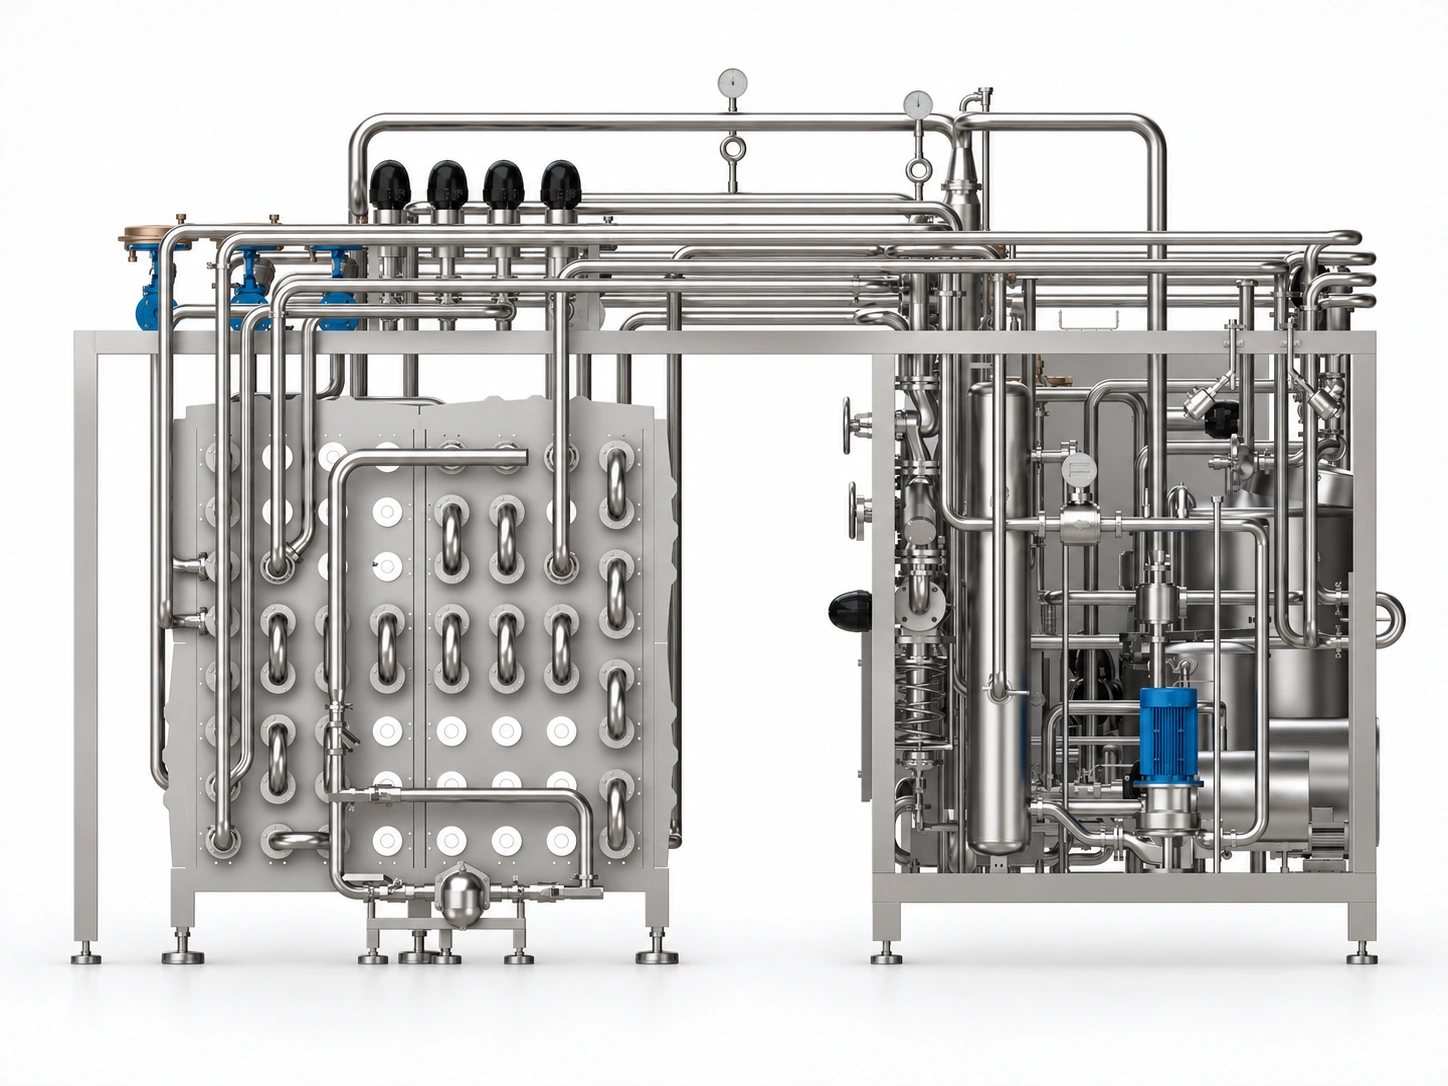
Rear view: tube bank, hot-water module and holding section.
UHT Plant Design, Cleaning and Integration
The right tube geometry, a validated sterilization cycle and smart cleaning decide how long and how reliably a UHT unit runs.
Each Protrus UHT unit is engineered from the product recipe. We select the tube type and diameter for the viscosity and particle size, set the heating profile for the required sterility, and size regeneration, hot-water and cooling sections for the capacity and the energy price at your site.
Tubular Heat Exchanger Designs
Multi-tube (shell and tube)
Several product tubes inside one shell carry the heating or cooling water. Compact, efficient and the standard choice for milk, flavored milk and plant-based drinks.
Tube-in-tube (annular)
Product flows in a wide annular gap. Suited to viscous products, desserts and drinks with fibers or small particles up to a few millimeters.
Corrugated tubes
A rolled wall profile creates turbulence at lower flow speed, which raises heat transfer and slows fouling. Expansion is taken up by floating ends with O-ring seals.

Top view: tube banks, steam valves, holding tube and pump group.
Sterilization, Cleaning and Automation
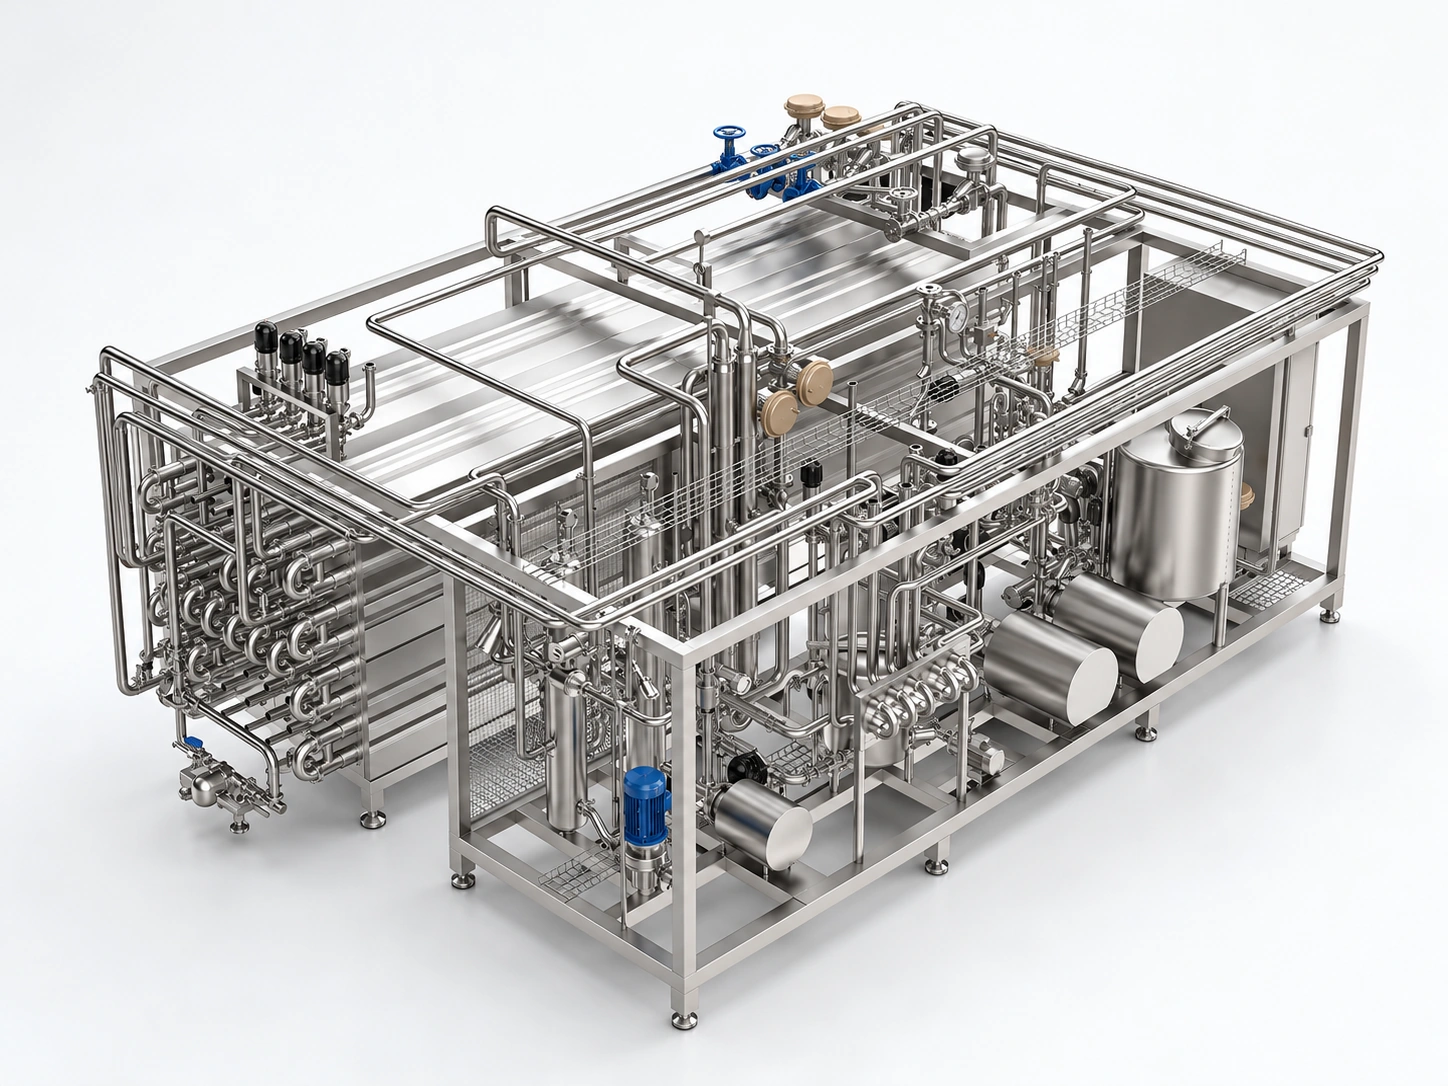
Isometric view: compact skid with service access on all sides.

Complete dairy with UHT unit: raw milk silos, mix and storage tanks, deaerator and CIP skids, homogenizer and the tubular UHT unit in the center.
Integration into a Complete Dairy
Protrus delivers the UHT unit alone or as part of a complete line: raw milk reception and silos, standardization, mix tanks for flavored milk and plant-based bases, homogenizer, UHT unit, aseptic tank, CIP and the piping to the aseptic filler of your choice.
One supplier is responsible for the process guarantee from the tanker to the package. See the full range of process technology for dairy.
Frequently Asked Questions About UHT Units
Have a question about your products, capacity or packaging? Ask our process engineers.
Get a Quote
Plan Your UHT Line with Protrus
Send us your products, hourly capacity, daily run time and packaging format. Our process engineers will define the heating profile, size the tubular heat exchanger, homogenizer, aseptic tank and utilities, and return a flow diagram, a 3D layout and a budget offer.
Prefer email? info@protrus.com